How Solar Panels Work
How solar panels work: the sun’s rays are small packets of energy called photons. See how cells, modules and strings turn light into output and what limits it.
The photovoltaic effect, without the physics lecture
A solar panel turns light into electricity. That sentence hides the part that matters for anyone inspecting a plant: the conversion happens inside a semiconductor, and it happens only where light reaches a working cell.
Sunlight arrives as photons. When a photon is absorbed by a silicon cell, it can free an electron. The cell is built with a positive and a negative layer, so the freed charges have somewhere to go: electrons collect on one side, the imbalance becomes voltage, and current flows once a circuit is closed. That is the photovoltaic effect.
Two consequences follow from that description. First, output depends on how much light reaches the cell: shading, soiling and snow reduce it directly. Second, output depends on the cell still being a working semiconductor: a cracked cell, a broken interconnect or a bypassed substring changes what the module can deliver, even in full sun.
From cell to module to string to array
The layers are worth keeping straight, because an inspection finding has to be located at the right one.
- Cell. The smallest converting unit. A module contains many of them, wired in series.
- Module (panel). Cells encapsulated behind glass, with a frame and a junction box. A common layout is six cells by ten, but the arrangement varies by manufacturer and is not part of the definition.
- String. Modules connected in series. Because they are in series, the weakest link in a string limits the current for that string.
- Array. The complete set of strings connected to the plant's inverters.
That series wiring explains a pattern inspectors see constantly: one shaded or faulty module can pull down the output of an entire string. It is also why a thermal camera is useful. A cell that is not converting behaves differently from its neighbors, and the difference is visible as temperature.
What limits output
Four factors decide how much a module produces on a given day.
- Irradiance. How much light reaches the plane of the module. This is the dominant variable and the reason two inspections on different days are not comparable without recording conditions.
- Temperature. Module efficiency drops as cell temperature rises. A hot, clear afternoon can produce less than a cool, bright morning on the same array.
- Shading and soiling. A shadow across one cell affects the whole string it belongs to. Dust, pollen, bird droppings and vegetation do the same thing gradually.
- Electrical condition. Cracks, corrosion, loose connectors, failed bypass diodes and insulation faults reduce what the module can deliver regardless of the weather.
The first three are environmental. They change between inspections and can be recorded. The fourth is the plant's condition, and that is what an inspection program is trying to track.
How failures show up
Failures rarely announce themselves as a dead module. More often they appear as a change in behavior.
- Thermal signature. A hot cell, a hot string or a warm junction box area suggests current is being forced through a path it should not take, or that a bypass diode is conducting.
- Visual damage. Cracked glass, discolored cells, snail trails, water ingress and frame corrosion are direct evidence, and RGB imagery is what documents them.
- Electrical measurement. An open circuit, a short, an insulation fault or a degraded curve shows up in measurement rather than in an image.
- Production data. Where string monitoring exists, a string producing consistently less than its neighbors is the earliest signal available.
None of these is conclusive on its own. A hot spot can be a defective cell or a leaf. A crack can be cosmetic or electrically significant. The value of an inspection workflow is that it puts the thermal image, the visual evidence and, where needed, the electrical measurement next to each other for the same module.
How inspection finds the problem
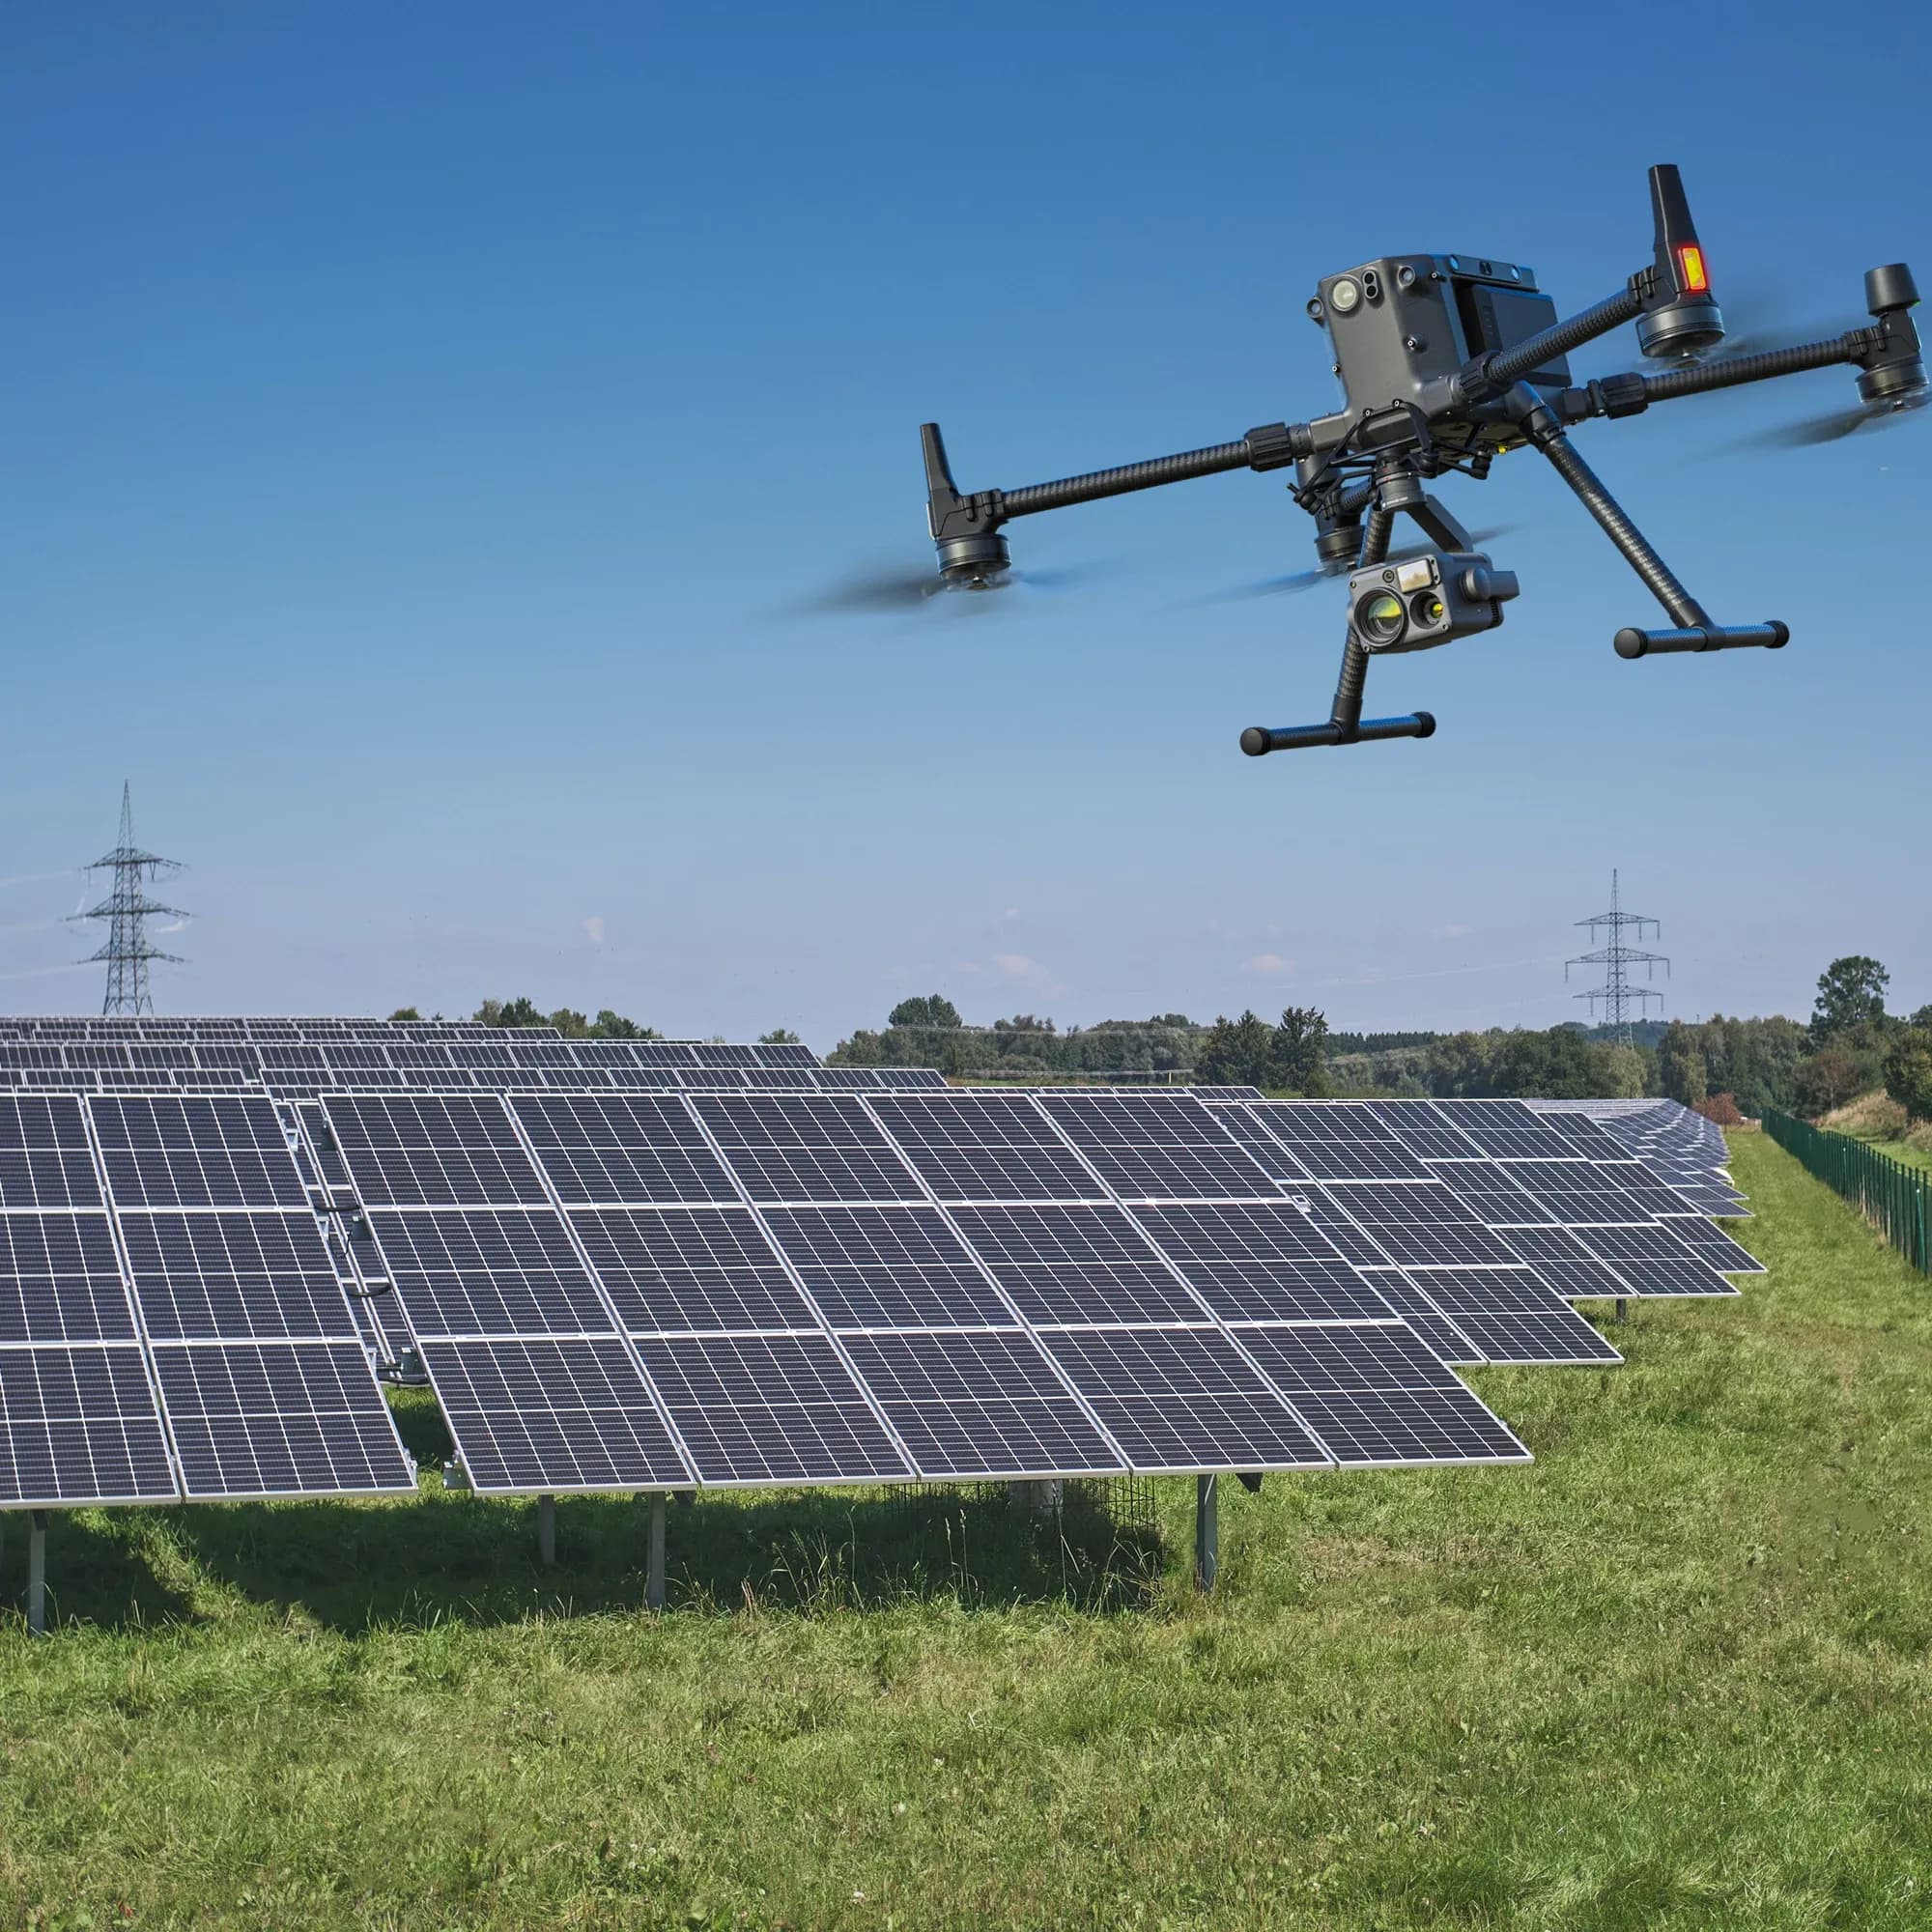
A drone-based inspection covers ground that would take a walking team days to cross. A thermal and RGB flight maps imagery onto module positions, and the review step turns candidates into findings.
The electrical layer answers a different question. IV curve tracing measures what the module actually delivers, insulation resistance and continuity tests describe the wiring, and short-circuit current measurements describe the string. These tests are slower and more intrusive, which is why they are targeted at modules and strings a thermal or production signal has already flagged.
Standards matter at the process level rather than the component level. IEC 62446-3 describes outdoor thermographic inspection of operating PV systems: equipment, conditions, procedure, competence and reporting. It does not turn a camera reading into a verdict; that comes from the review step and, where needed, the electrical test.
Reading a module over time
A module's condition is a history, not a snapshot. One inspection shows that a cell runs warm. A second inspection six months later shows whether it stayed the same, worsened, or improved after the module was replaced.
That comparison is only honest when the conditions are comparable, which is why the practical minimum for a repeatable record is: date and time, irradiance, module temperature, wind and cloud, flight parameters, plus the list of modules that could not be inspected. Without those, two thermal images can differ entirely because of the weather.
Over a few years, that record changes what a plant can do. Instead of replacing modules reactively, the maintenance team can see which failures repeat in the same area, a hint that the cause is environmental or installation-related rather than a defective batch.
What this means for maintenance decisions
Understanding the physics changes what you do with a finding.
If output drops across a string, the cause is likely something shared: shading, soiling, a connector, or a module dragging the series circuit down. If one cell runs hot while the string's output looks normal, the module is a candidate for inspection rather than immediate replacement. If a module fails an insulation or continuity test, that result, not the thermal image, is what drives the intervention.
Practical decisions follow the same order every time: locate the finding, verify it with the appropriate evidence, decide whether it changes safety, output or warranty exposure, and record what was done. Software's role in that chain is to keep the location and the evidence attached to the asset, so the next decision starts from what is already known.